

What "Body Style" Actually Means (and Why Port Size Rides Along)
Body style describes how many pressure-containing sections make up the valve and how you get at the trim. A 1-piece valve is a single shell. A 2-piece valve splits into a main body and an end cap. A 3-piece valve puts the working guts in a center section bolted between two end caps.
Most articles treat body style and port size as separate topics. They travel together. A 1-piece body forces the ball in through an end opening, so the ball has to be smaller than the connection and the bore comes out reduced. A 3-piece body opens up completely, so full port is the natural build. Pick a body style, and you've half-picked your port.
⚙️ Key Takeaways
- Match body style to maintenance needs
- Use 1-piece for disposable duty, 2-piece for general service, and 3-piece for welded or sanitary lines
- Choose full port for pigging or low pressure drop, and use reduced port for standard isolation
You're really making two decisions at once: how you'll service the valve, and how much pressure drop you'll tolerate. We'll put actual Cv numbers and a worked ΔP calculation on the port decision below, because almost nobody publishing on this topic does.
One note on vocabulary first. Metal ball valves for industrial service are built to API 608, pressure-temperature ratings come from ASME B16.34, and the pipe the valve lives in is governed by B31.1 for power piping or B31.3 for process piping. When a datasheet cites those documents, the ratings mean something. When it doesn't, ask why.
1-Piece Ball Valves: Cheapest to Buy, Impossible to Repair
A 1-piece valve is machined from a single casting or bar stock. The trim goes in through one of the end connections, which is why nearly every 1-piece design is reduced bore. There's no body joint to unbolt, and that cuts both ways.
The upside is honest. One body means one fewer external leak path than a 2-piece and two fewer than a 3-piece. On a compressed-air drop or a utility water branch, that simplicity is worth something.
The downside is permanent. A 1-piece valve can't be repaired, in line or on a bench. When the seats wear out, the valve is scrap. Treat these as consumables and price them that way.
Our recommendation is blunt: buy 1-piece valves only where nobody will ever service the line. That covers throwaway utility water and air, OEM equipment where the valve outlives the machine, and low-stakes drains. Put one on a process line, and you've scheduled a future outage.
2-Piece Ball Valves: The General-Purpose Workhorse

The differences between the three styles show up fastest in the 2-piece design. A main body and an end-cap section join by threads or bolts. That joint adds one potential external leak point, and in exchange you can open the valve and replace the internals.
Read the fine print on "repairable." A threaded-union 2-piece valve must come out of the pipe before you can rebuild it. On an NPT line with threads per ASME B1.20.1, that means draining the system, breaking the connections, and re-doping everything on reassembly. A bolted-flanged 2-piece is a different animal. Unbolt the flanges and the valve drops out cleanly, which puts it in genuine competition with 3-piece designs on flanged systems. Most competitor articles skip that nuance.
Compact 2-piece bodies in brass and stainless are the volume sellers of the industrial world, and quality builds carry high WOG ratings stamped right on the body. Check that stamped rating against your actual service pressure and temperature rather than trusting the nominal pipe class.
Where does the 2-piece belong? General industrial threaded service where the line can be drained and broken for maintenance, and where purchase price matters more than uptime. That describes most of the valves in most plants, which is why the 2-piece earns its workhorse label. Browse 2-piece ball valves
Not sure a 2-piece is the right call for a line you'll want to service later? Talk to a ValveMan engineer at 888-825-8800 — real engineers, not a call center.
3-Piece Ball Valves: When to Spend the Extra Money
In-Line Service Without Breaking the Pipe
Unbolt the center body of a 3-piece valve and the seats, ball, and stem come out while both end caps stay attached to the pipe. Alignment never moves. You swap a seat kit, torque the body bolts back down, and the line is back in service. No other body style does this.
The Welding Advantage Nobody Explains Properly

This case decides most 3-piece purchases. PTFE and RPTFE seats top out around 392°F. Welding temperatures blow past that by an order of magnitude. Socket weld or butt weld a 1-piece or 2-piece valve into a line and the heat cooks the soft seats trapped inside the body. You've destroyed the valve while installing it.
A 3-piece design solves this cleanly. Pull the center section, weld the two bare end caps into the pipe with the seats sitting safely on the bench, then bolt the center body back in. Years later, when those seats wear, the same trick works in reverse, and the welds never get touched.
A representative spec for this service is a 3-piece 316 stainless valve with socket-weld ends per ASME B16.11, rated 1000 psi WOG, with PTFE or RPTFE seats. Quality builds add a blowout-proof stem, which loads from inside the body so line pressure can't eject it. Put that on your checklist regardless of body style. Examples of these ball valves can be found here: stainless steel 3-piece ball valves, and we also have information on ball valve seat materials and temperature limits
Actuation and Total Cost of Ownership

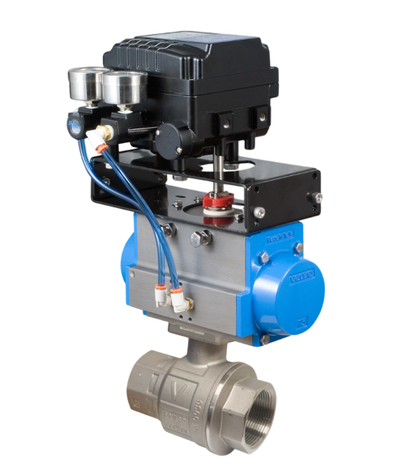
Many 3-piece bodies come with an ISO 5211 mounting pad cast or machined into the top works. That pad lets you bolt on a pneumatic or electric actuator later without touching the piping. If there's any chance the valve gets automated in the next decade, the pad costs you almost nothing today and saves a re-pipe tomorrow. You can learn more about our actuated ball valves here: actuated ball valves.
Now the money. A 3-piece valve costs more up front than a comparable 2-piece. Walk the failure scenario on a welded line and the math flips. With a 3-piece valve, a worn seat means a seat kit and roughly an hour of wrench time with the pipe intact. With a welded 2-piece, the same failure means cutting the old valve out, prepping and welding in a replacement, leak-testing the new joints, and eating the downtime for all of it, plus a certified welder on the clock. One avoided cut-out typically pays the entire body-style premium, and busy lines see more than one seat change over their life.
So when should you use a 3-piece? Use it on any welded line, full stop. Use it in food and beverage and pharma, where tri-clamp ends and frequent seat swaps for cleaning make in-line service routine. Use it in chemical processing, steam, and welded oil and gas lines where downtime is the biggest number on the invoice.
Spec'ing a valve for a welded or sanitary line? Call 888-825-8800 and get it right the first time — our engineers in Exton, PA will walk the failure math with you.
Full Port vs Reduced Port: The Cv Numbers Others Won't Give You

The definitions are simple. A full port valve has a ball bore matching the pipe ID, so the fluid never sees a restriction. A reduced-port valve runs a bore roughly one pipe size smaller, so a 3/4-inch valve carries about a 1/2-inch opening.
The penalty is quantifiable. A 3/4-port design cuts Cv roughly 30% versus full port; a 1/2-port design cuts it about 50%. At the same flow rate, that works out to roughly 2 to 4 times the pressure loss.
For water-like liquids, the estimate is one line of math: ΔP (psi) ≈ (Q/Cv)², with Q in gpm. Take a 1-inch valve with an illustrative full-port Cv of 40 and run 30 gpm of water through each port option, applying the 30% and 50% Cv reductions:
| Valve | Cv | ΔP at 30 gpm |
|---|---|---|
| 1" full port | 40 | 0.56 psi |
| 1" reduced (3/4-port), −30% Cv | 28 | 1.15 psi |
| 1" reduced (1/2-port), −50% Cv | 20 | 2.25 psi |
Read that table honestly. On a pump discharge line, a throttled branch, or ordinary on/off water and air service, an extra 0.6 to 1.7 psi disappears into the system noise, and the reduced-port body runs roughly 30% lighter and cheaper at the same pressure rating. Take the savings.
Full port becomes mandatory in specific duties. Pigged pipelines head the list, because a pig will jam solid in a reduced bore and turn a maintenance run into an excavation. Slurries and viscous media need the constant ID to keep solids moving. Gravity drains have no pump pressure to spend on a restriction, and cavitation-prone service punishes any velocity spike at the bore.
One rule from decades of field practice settles most small-bore arguments. In sizes below about 2 inches, the price gap between reduced and full port is often marginal, so buy full bore and delete the question from the spec review. The engineer who saved eight dollars on a reduced-port valve ahead of a future pig launcher has a story nobody wants to repeat. Here's more information on what Cv means and how to size a valve.
Selection Framework: Match Body Style and Port to the Job
| Service | Body style | Port | Why |
|---|---|---|---|
| Welded process line (SW or BW) | 3-piece | Full | Seats come out before welding; in-line rebuilds |
| Sanitary / food / pharma (tri-clamp) | 3-piece | Full | Frequent seat swaps for cleaning; no dead space |
| Flanged general industrial | Bolted 2-piece (3-piece if seats wear fast) | Size by Cv | Flanges give serviceability without the 3-piece premium |
| Threaded utility, maintainable | 2-piece | Size by Cv | Rebuildable once pulled; low cost |
| Throwaway utility water/air | 1-piece | Reduced | Cheapest install; replace on failure |
| Pigged, slurry, or drain duty | 2 or 3-piece per above | Full, mandatory | Constant ID keeps pigs and solids moving |
Run the port decision on numbers first. Compute ΔP = (Q/Cv)² at your design flow, compare it to what the system can spare, then check for pigging, slurry, or drain duty that forces full port regardless of the math.
Before the RFQ goes out, confirm each item on this list.
-
Specify the body material: 316SS for corrosives and sanitary work, brass for utility water and air, carbon steel where the piping code calls for it.
-
Specify the seat material and confirm its temperature limit against your process; PTFE-family seats end near 392°F.
-
State the required WOG rating and ask for API 608 and ASME B16.34 compliance on metal valves.
-
Call out the end connection standard: NPT per B1.20.1, socket weld per B16.11, flanged, or tri-clamp. Threaded vs flanged vs welded valve end connections
-
Require a blowout-proof stem.
-
Add an ISO 5211 mounting pad if there is any chance of actuation later.
Want a second set of eyes on that RFQ before it ships? Send it our way at 888-825-8800 or reach our valve experts. Five minutes now saves a warranty claim later.
Get the Right Body Style the First Time

The short version fits on an index card. A 1-piece valve is a consumable, a 2-piece is the workhorse for maintainable threaded and flanged lines, and a 3-piece is the uptime play for welded and sanitary service. Buy full port when pigging, solids, or the Cv math demand it, and pocket the savings on reduced port everywhere else.
Talk to a Real Valve Engineer
If the application has a wrinkle the tables above don't cover, call us at 888-825-8800 or reach our valve experts. You'll talk to real engineers in Exton, PA, not a call center. ValveMan has been matching valves to applications since 1965, and a five-minute conversation beats a warranty claim.