

Spec a gate valve where the line runs full open or full closed. Spec a globe valve anywhere you regulate flow. That is the whole decision rule, and the rest of this article shows you the geometry and the arithmetic behind it, because most comparison pages state the rule and then hedge it into mush.
The confusion is understandable. Both are linear-motion, multi-turn valves: a handwheel, a threaded stem, and several turns between open and closed. From the outside, a painted gate valve and a painted globe valve on a pipe rack can pass for cousins. Inside, they share almost nothing. The flow path through the body drives the Cv, the pressure drop, the erosion behavior, the flow-direction requirement, and the price. We covered the basics in our earlier post on the key differences between globe and gate valves; this one adds the numbers.
Inside the body: straight bore vs S-shaped flow path
A gate valve closes with a wedge that travels perpendicular to the pipe axis. Crank it open and the wedge retracts fully into the bonnet, leaving a straight, unobstructed bore through the body. Fluid passing through a fully open gate valve barely knows the valve is there. Wedges come in solid, flexible, and split variants, and the choice matters most in steam service, as covered below. Knife gates are a separate branch of the family, built with a thin plate that shears through slurries and pulp stock where a wedge would pack with solids.
A globe valve works the opposite way. The disc, sometimes called the plug, moves parallel to the flow and lands on a seat set horizontally inside the body. Fluid enters under the seat, turns 90 degrees up through the seat opening, passes the disc, and turns 90 degrees again to exit. That S-shaped path defines the type. It gives the disc a square, progressive landing on the seat, which makes precise flow regulation possible. It also costs pressure, and we can put a number on exactly how much.
Learn the part names before you call a distributor, because they carry real information: bonnet (the removable top housing), disc, seat, stem, backseat (the shoulder that seals the stem when the valve is fully open), and packing (the stem seal you will eventually service).
Body patterns: T, Y, and angle
The standard globe body is the T-pattern, with the seat horizontal and the stem vertical. The Y-pattern tilts the stem and seat roughly 45 degrees off the pipe axis, which straightens the flow path considerably. Y-pattern globes reduce pressure drop versus the T-pattern and are common in high-pressure, high-temperature power plant service for that reason. The angle pattern puts the inlet and outlet at 90 degrees, so the valve replaces an elbow in the piping layout while keeping globe-style trim.
Stem types and how to identify each valve in the field
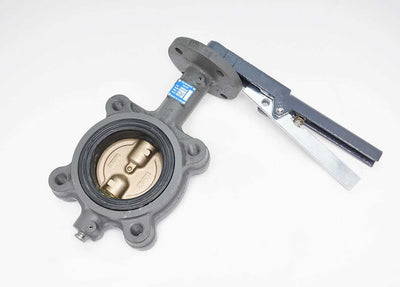
Gate valves come in rising-stem and non-rising-stem versions. On a rising-stem valve with an outside screw and yoke (OS&Y), the threaded stem climbs up through the yoke as you open it, so valve position is visible from across the room. In non-rising designs the gate travels on the threaded stem while the stem itself stays put, which suits buried service and tight headroom. In a mechanical room, the gate valve is the one with the slim, flat-sided body and the tall bonnet that houses the retracted wedge. The globe valve has a rounded, bulged body, and its handwheel takes fewer turns to stroke because the disc only travels the height of the seat opening.
Cv and pressure drop: the numbers that settle it
Cv is the flow coefficient: the number of US gallons per minute of 60°F water that passes through the valve at a 1 psi pressure drop. A bigger Cv means an easier path. Compare typical catalog values for the two types at equal size and the geometry argument turns into arithmetic.
| Size | Globe valve (typical Cv) | Gate valve (typical Cv) |
|---|---|---|
| 2 in | ~46 | ~200 |
| 4 in | ~195 | ~800 |
Treat these as representative catalog figures. Body pattern, trim, and manufacturer all move the number, so confirm against the data sheet for the actual valve you are buying before you size anything.
A worked example with ΔP = (Q/Cv)²
Pressure drop across a valve follows ΔP = (Q/Cv)², with Q in GPM and ΔP in psi for water. Run 300 GPM through a 4-inch gate valve with a Cv of 800. Divide: 300/800 = 0.375. Square it: 0.14 psi. Now run the same 300 GPM through a 4-inch globe valve at Cv 195. Divide: 300/195 = 1.54. Square it: 2.37 psi. Same pipe, same flow, and the globe valve eats about 17 times the pressure. That gap sits above the usual rule of thumb because the table pairs a high-Cv gate with a lower-Cv globe; across the common range, a fully open globe valve's S-path imposes roughly 3 to 10 times the pressure drop of an equal-size gate valve at the same flow. Run the same two-step arithmetic on your own flow rate and catalog Cv before you spec anything larger than a hose bibb.
What the extra drop costs over the life of the valve
That 2.23 psi difference never goes away. It is head your pump must supply every hour the line runs, which means motor load, which means a power bill. On a line that runs around the clock, a wide-open globe valve sitting where a gate valve belongs is a small tax you pay for decades. Where you genuinely need throttling at high flow, a Y-pattern globe recovers much of the penalty while keeping the seat-and-disc control that justifies the valve. That is our standing recommendation for steam and boiler-feed throttling: go Y-pattern and stop paying for a T-body's flow path.
Why throttling with a gate valve wrecks it
Crack a gate valve 20 percent open and you have built a crude orifice out of two precision sealing faces. The entire pressure drop concentrates across the narrow gap between the wedge and seat, and the resulting high-velocity jet erodes both surfaces. Machinists call the damage wire-draw, and it cuts channels into the seating faces that no amount of handwheel torque will close. The partially supported wedge also vibrates and chatters against its guides, which accelerates the wear.
Control is poor even before the damage starts. The flow area through a gate valve changes non-linearly with stem travel, so most of the flow change happens in a small fraction of the stroke and the rest of the handwheel turns do almost nothing. The end state is predictable: a gate valve that spent its life half-open eventually leaks at shutoff, so it fails at the one job it was specced to do.
A globe valve used purely for on/off isolation works fine mechanically. It simply pays that 3–10x pressure penalty forever. Match the valve to the duty and you avoid both failure modes.
Flow direction, installation, and water hammer
Gate valves are bi-directional and install in either orientation. Globe valves are unidirectional, with a flow arrow cast into the body, and ignoring that arrow is one of the most common field errors we hear about. The standard orientation puts flow under the disc, so line pressure helps lift the plug on opening and the packing sits on the low-pressure side when the valve is shut. Install a globe valve backwards and the symptoms show up fast: the disc chatters at partial openings, and the handwheel fights you on opening because line pressure now pushes the disc onto the seat.
Both types share one quiet installation advantage. Closing takes multiple handwheel turns, so neither valve can be slammed shut the way a quarter-turn ball or butterfly valve can. On a long liquid line, that slow closure limits the pressure surge of water hammer, and it is a legitimate reason to keep multi-turn valves on services where an operator in a hurry could otherwise bang a column of water to a stop.
Standards, materials, and shutoff class
Write the spec against the documents buyers and inspectors actually use. API 600 covers bolted-bonnet steel gate valves for petroleum and process service, and API 602 covers the compact forged gate valves common in small-bore steel piping. On the iron side, MSS SP-70 governs cast iron gate valves and MSS SP-85 governs cast iron globe valves. ASME B16.34 sets the pressure-temperature class ratings that tell you what a Class 150 or Class 300 body actually holds at your operating temperature.
On shutoff, be honest with yourself. Metal-seated gate and globe valves typically test in the API 598 Class IV–V leakage range, and neither matches a soft-seated ball valve for bubble-tight shutoff. If your service demands zero visible leakage on clean, compatible media, a soft-seated ball valve is the better isolation tool, and the gate-vs-globe question becomes moot.
Material selection follows the media. Bronze bodies handle domestic water and HVAC duty. WCB cast carbon steel is the workhorse for steam and general process service. Stainless trim and bodies go on corrosives, and sour hydrocarbon service calls for trim qualified to NACE MR0175. Two steam-specific notes earn their place here because almost nobody else publishes them. A solid-wedge gate valve closed hot can bind in its seats as the body cools and contracts around it, and the flexible wedge exists specifically to absorb that seat movement. Liquid trapped between the double seats of a closed gate valve can overpressure the bonnet cavity when the line heats up, so blocked-in services on temperature-swinging lines need a relief provision in the design.
Applications, actuation, and cost
The duty map writes itself once the rule is in hand. OS&Y gate valves dominate water mains and fire protection service, where the visible stem tells an inspector at a glance whether the valve is open. Y-pattern globes carry boiler feed and steam throttling in power and process plants. T-pattern globes handle fuel oil regulation and cooling-water balancing. Gates block pipelines and pump suction and discharge, where they sit fully open for years at a time.
Automation on multi-turn valves takes specific hardware. Large gates and globes get gear operators to cut handwheel effort, and powered service means an electric multi-turn actuator that can drive the stem through its full thread travel. The rack-and-pinion pneumatic actuators that bolt onto ball valves rotate 90 degrees and stop, so they have no business on a multi-turn stem; budget for the right actuator type from the start.
On price, the gate valve wins at equal size and pressure class because its construction is simpler. Ownership cost flips the ranking. A globe valve idling wide open in a high-flow line costs you pump energy every hour, and a gate valve throttled to death costs you a replacement valve plus the downtime to swap it. The cheapest valve is the one matched to its duty.
The selection checklist
- Settle the duty first, because it decides most cases alone: isolation points to a gate valve, regulation points to a globe valve.
- Run ΔP = (Q/Cv)² at your actual flow rate before you commit, and check the result against the pressure budget for the line.
- Count the cycles, since a valve that strokes daily lives a different life than one that moves twice a year.
- Confirm whether flow direction is fixed, because a reversing line rules out a standard globe valve.
- Match the pressure class and temperature to the ASME B16.34 rating, using the operating temperature rather than ambient.
- Pick body and trim materials for the media, including NACE MR0175 trim if the service is sour.
- Decide on actuation now, even if the actuator comes later, so the stem and mounting suit a gear operator or electric multi-turn drive.
- Leave maintenance access above the bonnet for repacking and seat work, because every stem packing eventually needs attention.
Sixty-plus years of sizing these valves has taught us that most bad installs trace back to skipping step one. If you want a second set of eyes on the spec, send the line conditions to the Exton, PA team through our contact page or call 888-825-8800 and talk it through before you buy.